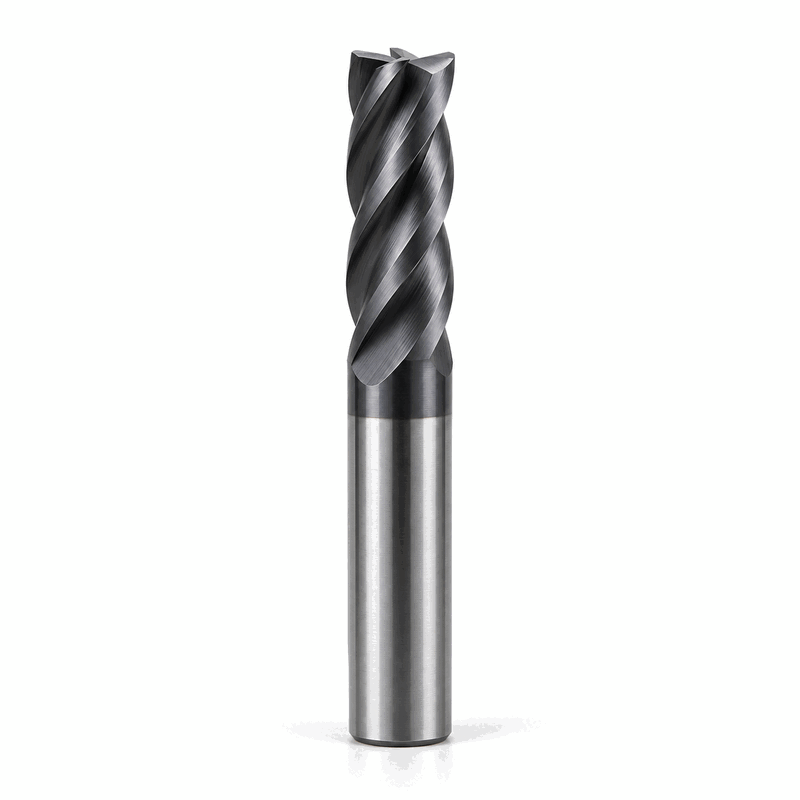
Solutions by material
Steel
Dụng cụ và thông số gia công phù hợp với Thép.
Solutions by material
Steel
Dụng cụ và thông số gia công phù hợp với Thép.
- Carbon steel
- Alloy steel
- Structural steel
- Tool steel
Approved cutting data
ISO group P.
Starting values must be adjusted for hardness, machine and setup.
| Operation | Tool type | Hardness | Vc | fz | ap / ae | Source |
|---|---|---|---|---|---|---|
| Carbide end mill | Carbide end mill | 120 - 220 | 0.03 - 0.12 | 1 - 3 | Steel < 45 HRC | |
| Carbide drill | Carbide drill | 80 - 150 | 0.05 - 0.20 | — | Reduce Vc by 20% for deep holes | |
| Turning insert | Turning insert | 150 - 300 | 0.10 - 0.30 | 0.5 - 3.0 | Depends on the operation | |
| Tapping | Tapping | 10 - 30 | — | — | Use suitable cutting fluid |
Technical advice
Get advice ↗Need help choosing?
Send your material, machine and machining conditions for our engineers to propose a solution.